A Successful Presence at Dairy Expo 2026
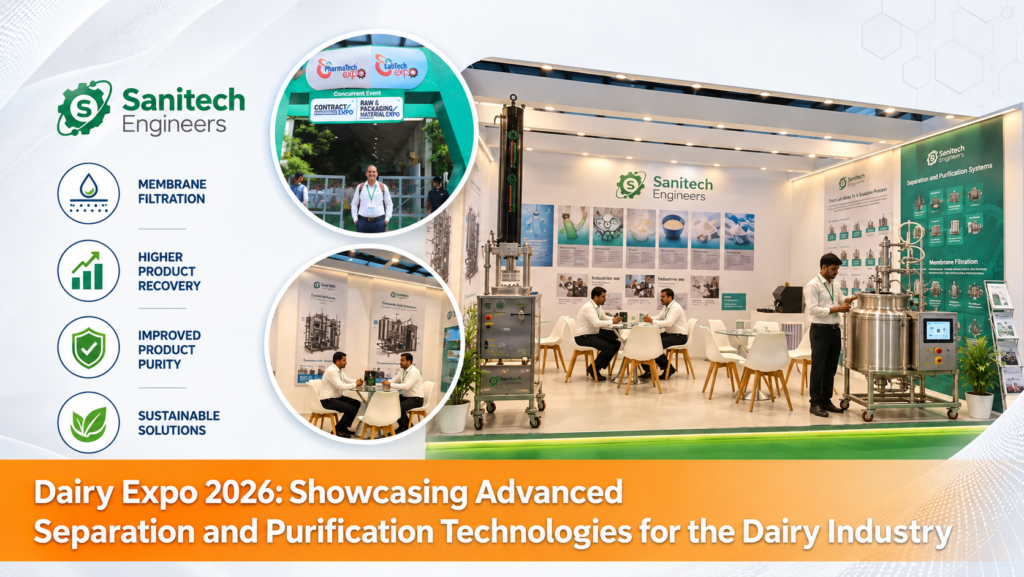
Dairy Expo 2026 provided an excellent opportunity for Sanitech Engineers to engage with dairy manufacturers, industry experts, technology partners, and processing professionals from across the sector. Over three insightful days, we exchanged ideas, explored emerging industry trends, and demonstrated how advanced separation and purification technologies are helping dairy processors improve efficiency, product quality, and sustainability.
Everyone who visited our booth and took the time to discuss their processing challenges and future growth plans. The conversations reaffirmed the industry’s increasing focus on maximizing product recovery, enhancing product purity, reducing operational costs, and adopting sustainable manufacturing practices.
Supporting the Dairy Industry Through Membrane Filtration Technologies
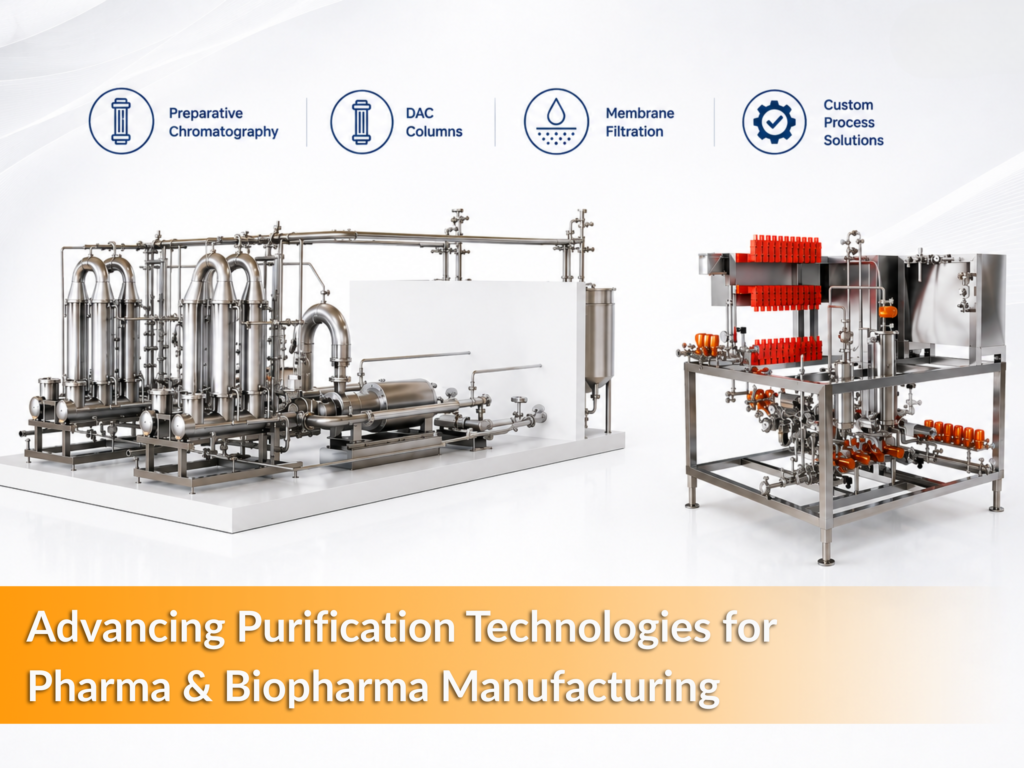
As one of India’s leading manufacturers of membrane filtration and preparative chromatography systems, Sanitech Engineers specializes in delivering customized separation and purification solutions for the dairy industry.
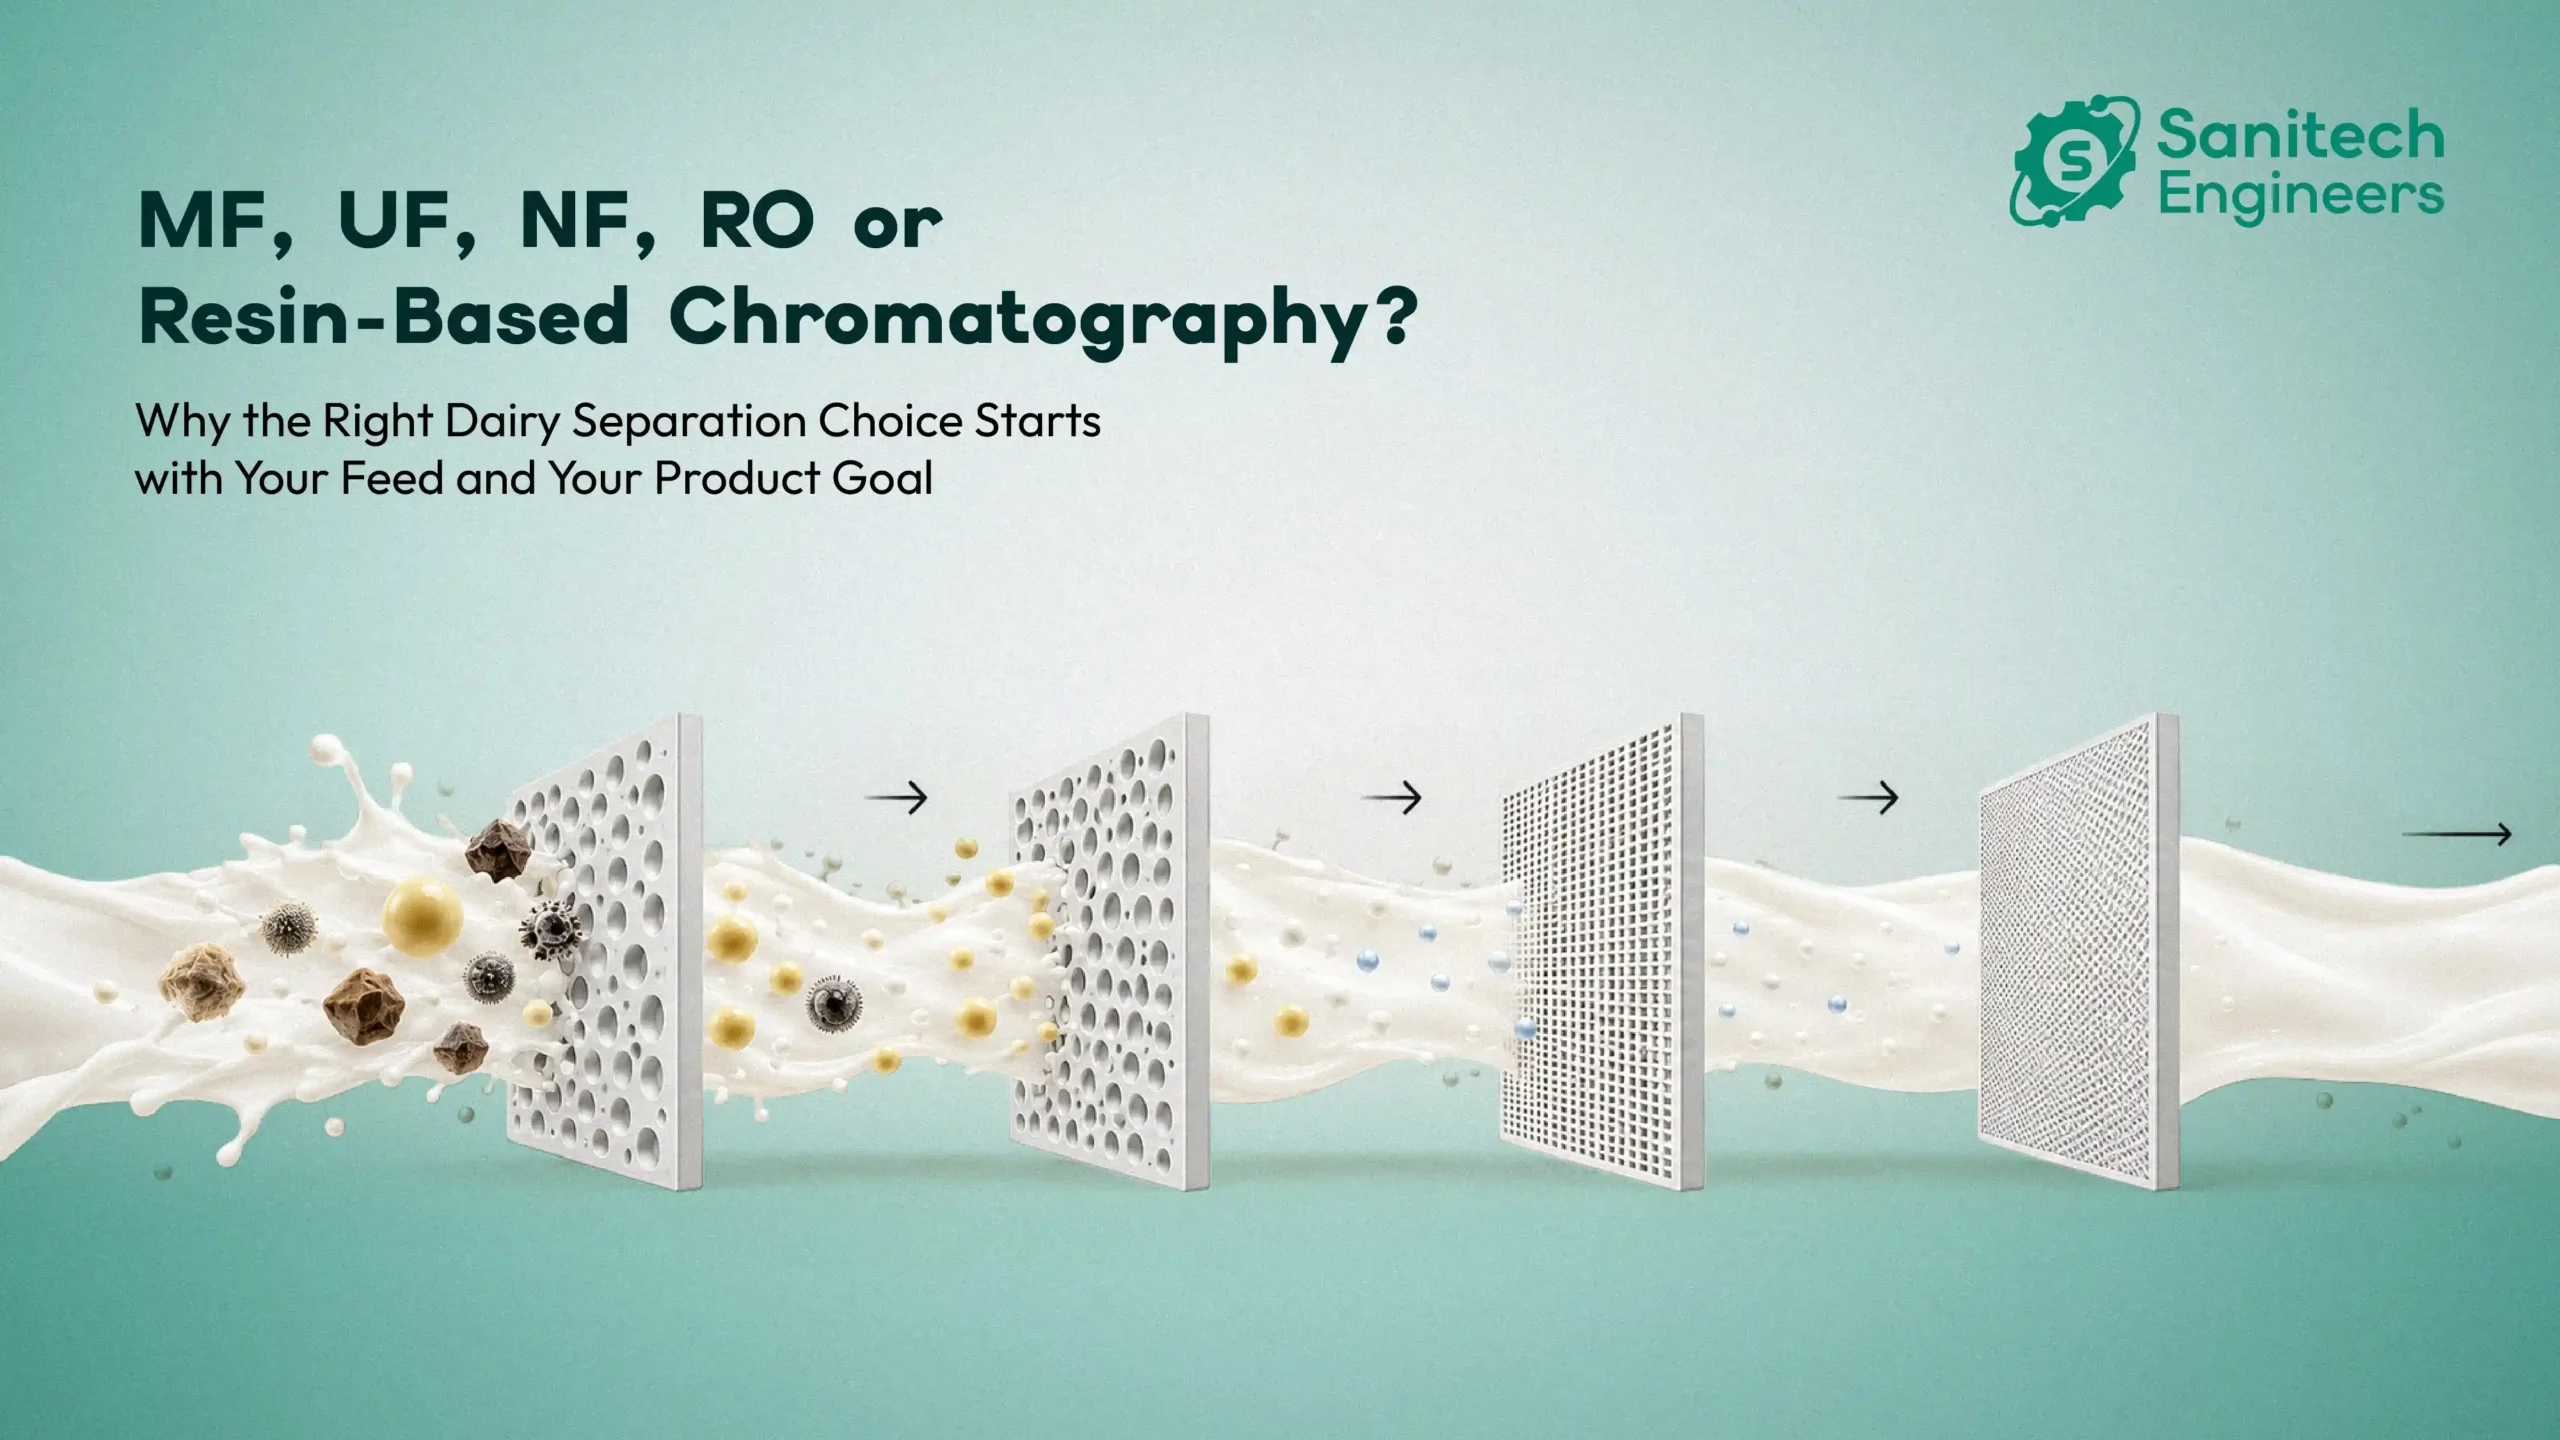
At Dairy Expo 2026, we showcased about our advanced membrane-based technologies, including:
- Microfiltration (MF) Systems
- Ultrafiltration (UF) Systems
- Nanofiltration (NF) Systems
- Reverse Osmosis (RO) Systems
- Ion Exchange Systems
- Whey Demineralization Solutions
- Whey Protein Concentration (WPC) Systems
- Milk Protein Concentration (MPC) Systems
- Lactose Recovery and Concentration Solutions
These technologies enable dairy manufacturers to optimize production processes, recover valuable dairy components, improve product consistency, and create high-value dairy ingredients while reducing waste generation.
Driving Product Recovery and Product Purity
Today’s dairy industry demands more than just increased production capacity. Manufacturers are increasingly focused on extracting maximum value from every process stream.
Advanced membrane filtration and purification systems help achieve:
- Higher whey protein recovery
- Efficient lactose concentration
- Whey demineralization for infant nutrition applications
- Improved milk and whey protein concentration
- Reduced energy consumption
- Enhanced process efficiency
- Sustainable resource utilization
- Consistent product quality
By integrating modern separation technologies into dairy operations, manufacturers can achieve greater operational efficiency while meeting evolving market and regulatory requirements.
Innovation Through Separation and Purification
The future of dairy processing lies in intelligent process design and advanced separation technologies. Membrane filtration systems have become essential tools for dairy processors looking to improve yields, reduce environmental impact, and produce value-added products.
At Sanitech Engineers, our focus remains on delivering customized membrane filtration and purification solutions that help customers achieve superior product quality, improved product recovery, and long-term operational excellence.